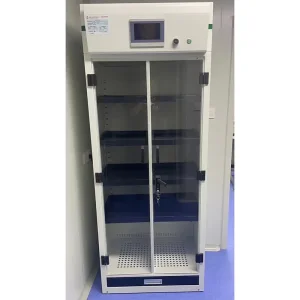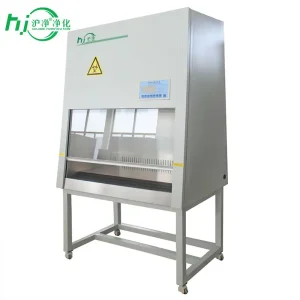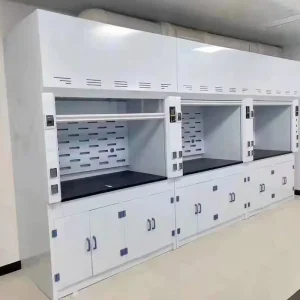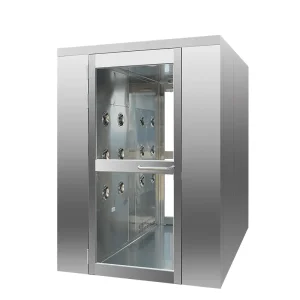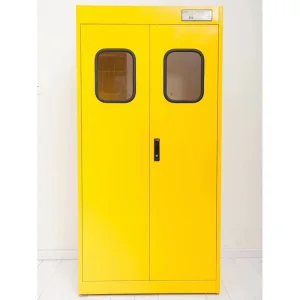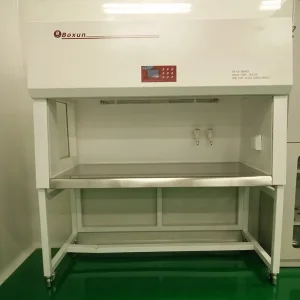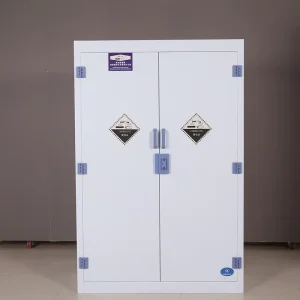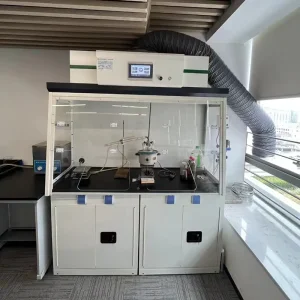
The global demand for high-end Medicine Cabinets for Pharmacy and laboratory storage has seen an unprecedented shift. As regulatory requirements (ISO, FDA, GMP) tighten, suppliers in China have evolved from simple manufacturers to high-tech solution providers. We specialize in providing the structural backbone for global pharmaceutical and clinical R&D.
Future Roadmap: The industry is transitioning towards "Smart Storage," incorporating IoT sensors for real-time temperature monitoring, air purification, and inventory tracking. Our manufacturing facility in Nantong integrates these technologies to ensure our clients receive not just a cabinet, but a comprehensive hazard-mitigation solution.
With 20+ years of manufacturing experience, our company stands at the intersection of material science and clinical safety. Established in 2004, our 10,000m² facility reflects our commitment to the E-E-A-T principle (Experience, Expertise, Authoritativeness, and Trustworthiness). We don't just supply products; we provide verified industrial assets that comply with international safety standards.
China offers a matured manufacturing supply chain, allowing for the customization of safety cabinets that meet both local regulations and international ISO requirements at high cost-efficiency.
We utilize corrosion-resistant, high-grade cold-rolled steel with electrostatic powder coating, tested under extreme chemical exposure environments.